简体中文
 English
How to Use a Wire Rope Breaking Strength Table
The table value is a lower bound, not an average; K and fill factor set how much steel fits in a diameter
What the number in the table means
A breaking strength table usually gives the minimum breaking force, not an average measured from one rope. It is the lower limit a rope made to the standard must reach in test; below it, the product does not conform.
Table values are arranged by construction, diameter and wire tensile grade. In one row, a larger diameter or a higher grade gives a higher breaking force; in one column, differences between constructions come from metallic area and the way the rope is laid.
Before reading the table, confirm three things: the construction code is the same class, the diameter is the nominal diameter, and the grade is the same grade. If any one differs, the numbers cannot be compared directly.
Breaking forces for common constructions and diameters can be compared in the wire rope breaking strength table
The breaking force formula and the K factor
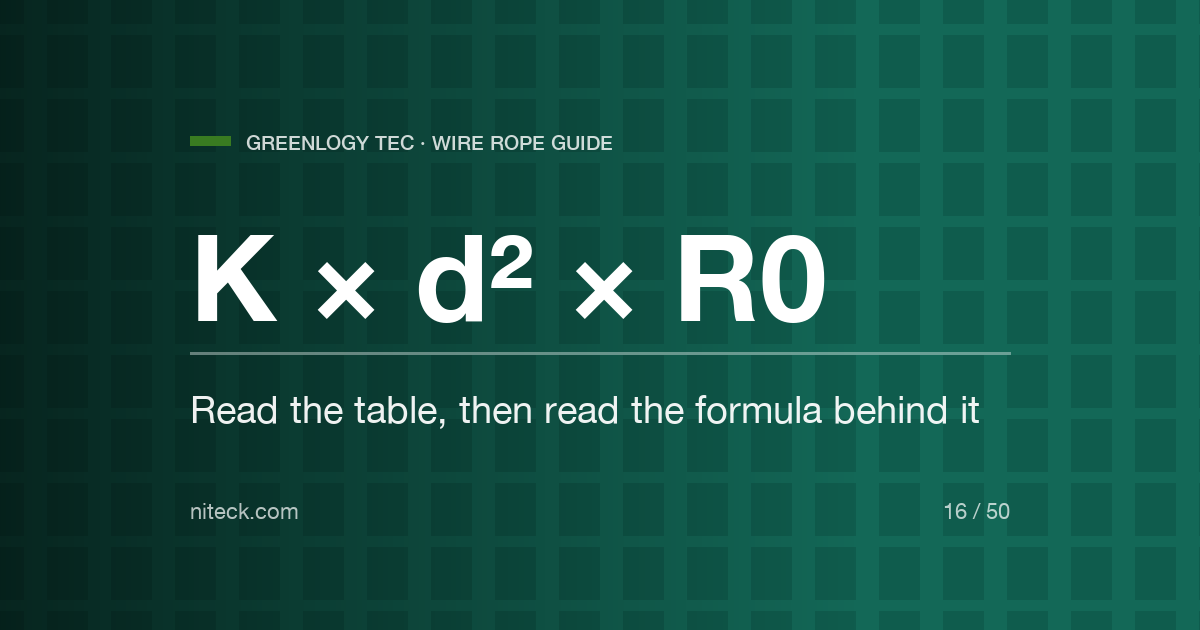
Engineering practice uses a simplified formula to estimate minimum breaking force: F0 equals K times d squared, times R0, divided by 1000. F0 is in kilonewtons, d is the nominal rope diameter in millimetres, and R0 is the wire tensile grade in megapascals.
K is an empirical factor that folds in metallic area, lay angle and lay length. It is not a fixed constant: different constructions and different standards give different K values, and the same construction may take a different value under another standard.
When estimating, use the nominal diameter and the nominal wire grade. The result should sit close to the table value; a large difference usually means the wrong construction or grade was used, or that compacted or sealed strand coefficients were applied to an ordinary rope.
The formula is for estimation and checking only. Formal design must use the minimum breaking force in the product standard or the maker's data; an estimate does not replace a guaranteed value.
Fill factor decides how much steel fits in a diameter
Fill factor is the total steel cross-section in the rope divided by the circle area calculated from the nominal diameter. The higher the fill factor, the more steel in the same diameter and the higher the breaking force.
An ordinary 6x19 class construction usually has a fill factor between about 0.4 and 0.5; compacted, sealed and filler constructions pack more wire into the same circle and reach a higher figure. That is why a compacted rope carries a higher breaking force than an ordinary rope at the same diameter.
Fill factor also affects weight and bending behaviour. More steel means a heavier rope and greater deformation of the outer layer in bending; at equal breaking force a high-fill rope can use a smaller diameter, but its bending fatigue performance is not necessarily better. Do not select on breaking force alone.
Fill factor and K value are two ways of saying the same thing: a high K usually means a high fill factor or efficient laying. When two table values differ for the same construction and grade, ask about construction detail and laying method first.
Different standards, different table values
GB/T 8918, ISO 2408 and ASTM A1023 all give minimum breaking forces, but their construction classes, diameter series and tensile grades are not identical. The same rope looked up under different standards can give different numbers.
The differences come from several places: the method of calculating metallic area, the laying efficiency assumed, the series of tensile grades, and whether certain special constructions are included. Some standards publish one table by rope class; others give values by construction and grade.
Put the standard into the purchase order. With only construction, diameter and grade stated, minimum breaking forces under different standards can differ by a whole step; state up front which standard will govern acceptance as well.
Nominal data and construction codes for the main standards are listed in the steel wire rope data tables
Minimum breaking force versus actual breaking force
Minimum breaking force is a guaranteed value; actual breaking force is usually higher. A type test or sample test may measure a few percent above the table value, and results scatter with specimen, gripping and test method.
Design on the minimum, not on the measured average. Designing on an average puts half the production outside the safety margin; designing on the minimum keeps even the weaker ropes in a batch inside it.
The safety factor is a separate layer. Equipment codes give a safety factor by application; minimum breaking force divided by that factor gives the allowable pull. Write the relationship between safety factor, breaking force and actual load into the design file.
If the customer wants a measured breaking force, the order must state the test method, specimen length, gripping method and acceptance rule. Results from different methods cannot be compared directly.
The order of using the table
First fix the application and the safety factor and calculate the required allowable pull; multiply by the safety factor to get the required minimum breaking force; then look up the table by construction and diameter and find the smallest size that meets it.
Prefer standard constructions when reading the table, and confirm special ones separately. Values for compacted, sealed and rotation-resistant ropes cannot be taken from an ordinary construction; use the table or maker's data for that construction.
After choosing the size, check the rest: whether sheave and drum D/d are satisfied, whether capacity is enough, whether the termination can carry the load, and whether the weight is inside the equipment limit. Meeting the breaking force is only the first step.
The link between construction and minimum sheave diameter is set out in the wire rope construction guide
Common mistakes
The first mistake is treating breaking force as allowable pull. Breaking force is the load at which the rope breaks; allowable pull is that value divided by a safety factor, and the two differ by several times.
The second is mixing standards. Pairing an ISO table value with a GB rope, or an ordinary construction value with a compacted rope, miscalculates the margin.
The third is ignoring diameter tolerance. The actual diameter may be larger than nominal, so area and weight rise, but the breaking force is still guaranteed on the nominal figure; back-calculating area from the actual diameter overstates capacity.
The fourth is comparing price without comparing standard. Two ropes both marked 6x19 and 1770 can be entirely different products under different standards and fill factors. A quotation that states the standard and minimum breaking force is far more useful than a construction code alone.
One-line rule
A breaking strength table is the start of selection, not the end. Confirm construction, diameter, grade and standard first, check with the formula or the table next, and finish by checking D/d, capacity and termination conditions.
The table gives a lower bound, design works to the limit, and acceptance judges against the standard. Keep those three separate and written down, and selection and acceptance will not contradict each other; a construction code alone often delivers a guaranteed value other than the one you assumed.